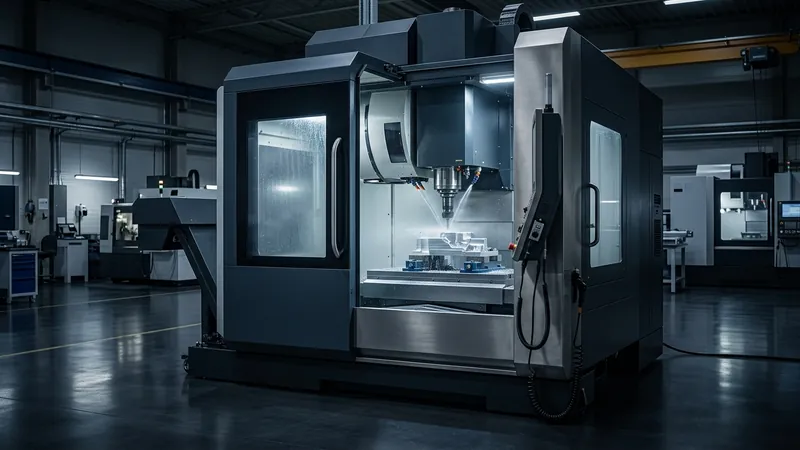
When selecting between a slant-bed CNC lathe (such as the Taikan TCK50, TCK52, or TCK56) and a horizontal flat-bed CNC lathe (such as the CK6140, CK6150, or CK6160), the main selection factors are batch volume, workpiece length-to-diameter ratio, and chip load intensity. A 45° one-piece slant-bed CNC turning center uses preloaded roller linear guideways (24 m/min rapid traverse) and a 12-station servo turret (0.2 s indexing) to reduce cycle times by 30% to 45% on medium-to-high volume chucking and bar-fed components up to Ø460 × 750 mm, while maintaining ±0.002 mm repeatability through gravity-assisted chip evacuation. Conversely, a horizontal flat-bed CNC lathe features wide ultrasonic-quenched cast-iron bedways (330–400 mm width, HRC 52–55) and a 3-step geared headstock with large spindle bores (Ø52 to Ø105 mm), offering 25%–35% lower initial capital cost and superior support for long shafts (1,000 to 3,000 mm between centers) and heavy oilfield pipe threading.
Summary
- · Choose a 45° Slant-Bed Lathe (TCK50 / TCK52 / TCK56) when annual batch sizes exceed 1,500 parts, when integrating a bar feeder (Ø52–Ø78 mm), or when holding IT6 tolerances (±0.004 mm positioning, ±0.002 mm repeatability).
- · Choose a Horizontal Flat-Bed Lathe (CK6140 / CK6150 / CK6160) when turning shafts between 1,000 mm and 3,000 mm long, machining Ø600 mm large-swing flanges at low RPM, or passing Ø82–Ø105 mm pipes through the spindle.
- · Gravity chip evacuation on a 45° slant bed prevents hot steel swarf from resting on the Z-axis guideways, cutting thermal Z/X diameter drift by more than 60% over an 8-hour shift.
1. Structural Mechanics: 45° one-piece Slant Bed vs. Quenched Flat Bedways
The geometry of a CNC lathe bed dictates how tangential and radial cutting vectors are transferred into the shop foundation. On a 45° one-piece slant-bed turning center like the Taikan TCK52 or TCK56, the resultant cutting force vector during outside-diameter (OD) turning points downward and inward between the two guideway rails. This places the Fine-Grain HT300 casting under pure compression rather than cantilevered bending.
By contrast, a horizontal flat-bed CNC lathe (CK6140, CK6150, CK6160) places its wide V-and-flat induction-hardened ways (330 mm to 400 mm wide) in a horizontal plane. When turning heavy 1.5-meter to 3-meter shafts between centers with a steady rest, the flat bed provides an exceptionally stable horizontal datum for setting up heavy tailstocks, roller steady rests, and large 4-jaw independent chucks.
In continuous dry or heavy-coolant turning of 4140 alloy steel, hot chips accumulating on a horizontal bed transfer heat directly into the saddle. A 45° slant bed drops 95% of swarf straight into the side conveyor pan within 1.5 seconds of chip formation.
2. Engineering Specification Matrix: TCK Series vs. CK Series
To match your part drawings to the optimal machine architecture, compare the structural and kinematic envelopes of our six CNC turning platforms below:
| Engineering Parameter | TCK50 / TCK52 / TCK56 (Slant Bed) | CK6140 / CK6150 / CK6160 (Flat Bed) |
|---|---|---|
| Bed Architecture | 45° One-Piece one-piece HT300 Casting | Horizontal HT300 Bed, Quenched HRC 52–55 |
| Max Turning Diameter | Ø360 mm / Ø400 mm / Ø460 mm | Ø400 mm / Ø500 mm / Ø600 mm Swing |
| Max Workpiece Length | 500 mm / 550 mm / 750 mm | 750 mm to 3,000 mm Between Centers |
| Through-Spindle Bore | Ø62 mm / Ø76 mm / Ø90 mm | Ø52 mm / Ø82 mm / Ø105 mm |
| Rapid Traverse (X / Z) | 24 / 24 m/min (Roller Linear Ways) | 6 / 8 to 6 / 10 m/min (Turcite-B Box Ways) |
| Tool Turret Indexing | 8 or 12-Station Servo (0.2 s) / BMT Live | 4-Station Electric or 6/8-Station Horizontal |
| Repeatability (ISO 230-2) | ±0.002 mm | ±0.004 mm |
3. Cycle-Time & Total Cost of Ownership (TCO) Calculation
Consider a typical automotive flanged transmission shaft (42CrMo4 alloy steel, Ø95 × 280 mm) requiring rough OD turning, finish profiling, grooving, internal boring, and M24 threading (5 tools total).
On a CK6140 flat-bed lathe with a 4-station electric tool post and 8 m/min rapids, non-cutting tool change and approach time consumes 28 seconds per part, yielding a total floor-to-floor cycle time of 142 seconds. On a TCK50 slant-bed turning center with a 12-station 0.2-second servo turret, 24 m/min rapid traverse, and hydraulic chuck foot-pedal actuation, total cycle time drops to 86 seconds, a 39.4% throughput increase.
- · High-Mix / Long-Shaft Job Shops (<50 pcs/lot, lengths >800 mm): CK6150 or CK6160 achieves full capital payback 5 months faster due to lower initial acquisition cost and zero custom fixturing.
- · Medium-to-High Volume Production (>200 pcs/lot, bar-fed or chucked parts <750 mm): TCK50, TCK52, or TCK56 generates $18,000–$32,000 in additional annual spindle revenue per shift while reducing scrap rates via ±0.002 mm repeatability.