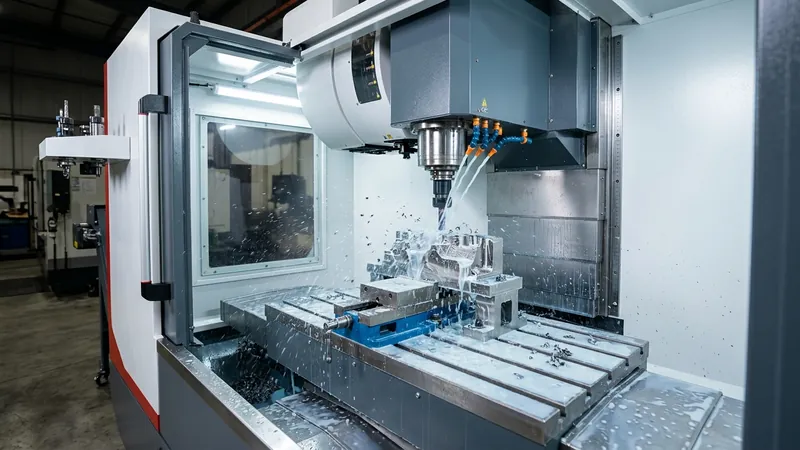
Hard turning on a rigid slant-bed CNC lathe using Cubic Boron Nitride (CBN) inserts machines heat-treated steel components (55–62 HRC) directly to final tolerances in a single clamping setup, frequently replacing conventional cylindrical grinding. While cylindrical grinding remains necessary for ultra-fine surface finishes below Ra 0.15 µm or extreme roundness under 0.001 mm, hard turning on a one-piece 45-degree slant-bed lathe like the TCK52 or TCK56 achieves Ra 0.25–0.40 µm surface roughness and IT5–IT6 dimensional accuracy. By eliminating secondary grinding machines, coolant sludge filtration systems, and wheel dressing downtime, manufacturers reduce capital expenditure by 40% and shorten per-part cycle times by 50% to 70% on complex contours, bores, and faces.
Summary
- · Hard turning achieves Ra 0.25–0.40 µm and IT5/IT6 accuracy on 58–62 HRC alloy steels in a single setup.
- · Single-point CBN tooling machines OD, ID, tapers, and shoulders simultaneously without custom profile grinding wheels.
- · High dynamic stiffness, found in the TCK52 and TCK56 45° slant-bed castings, is the #1 requirement to prevent CBN insert micro-chipping.
1. Why Manufacturers Are Replacing Grinding Cells with Hard Turning
Traditionally, machining bearing races, transmission shafts, and hydraulic spools above 55 HRC required rough turning in the soft state, heat treatment, and multiple cylindrical grinding setups for outer diameters, inner bores, and shoulders.
With modern PCBN (Polycrystalline Cubic Boron Nitride) tooling and high-rigidity slant-bed CNC lathes, production engineers can finish-machine hardened components in a single chucking, improving concentricity between bores and outer journals.
Hard turning generates high radial passive forces. Attempting hard turning on lightweight lathes causes chatter and rapid CBN edge fracture. Always specify a heavy one-piece HT300 slant-bed casting with preloaded roller guideways.
2. Hard Turning vs. Cylindrical Grinding: Direct Engineering Comparison
Evaluate the technical and financial trade-offs between CBN hard turning on our TCK52/TCK56 platforms and traditional cylindrical grinding:
| Process Metric | CBN Hard Turning (TCK52 / TCK56) | Conventional Cylindrical Grinding |
|---|---|---|
| Achievable Surface Finish | Ra 0.25 – 0.40 µm | Ra 0.05 – 0.20 µm |
| Dimensional Tolerance Grade | IT5 – IT6 (±0.003 to ±0.005 mm) | IT4 – IT5 (±0.001 to ±0.003 mm) |
| Multi-Surface Capability | OD, ID, face, taper & thread in 1 setup | Requires separate OD/ID grinders or wheel changes |
| Material Removal Rate | 3x to 5x faster than grinding | Limited by wheel burn threshold |
| Coolant & Environmental Cost | Dry cutting or low-mist MQL (clean chips) | Heavy flood coolant + hazardous grinding swarf filtration |
| Equipment CAPEX & Footprint | Baseline (1 compact lathe) | 1.8x – 2.5x higher CAPEX and floor space |
3. Recommended Taikan Machine Configurations for Hard Turning
To guarantee repeatable micron-level tolerances when turning hardened steel, we configure our slant-bed lathes with three critical mechanical upgrades:
- · TCK52 for Medium Hardened Rings & Shafts (up to Ø380 mm): 8-inch hydraulic chuck, P4 ultra-precision angular contact spindle bearings, and C3 ball screws.
- · TCK56 for Large Hardened Gears & Sleeves (up to Ø420 mm): 10-inch hydraulic chuck, 15 kW high-torque spindle drive, and 45 mm roller linear guideways.
- · Rigid Hydraulic Turret Clamping: High-force curvic coupling turret locks toolholders with zero deflection under radial passive cutting loads.