To obtain an accurate CNC lathe or vertical machining center quotation within 24 hours, engineering procurement teams should provide seven core parameters: 2D part drawings with geometric tolerances (GD&T) and 3D STEP models, raw material grade and hardness (HRC or HB), blank state (bar stock, forging, or casting), target surface roughness (Ra/Rz), annual production volume or target takt time, fixture and tailstock preferences, and facility electrical/pneumatic standards. Supplying these parameters allows application engineers to select the exact machine frame (such as a TCK50 slant-bed lathe for bar work or a CK6150 flat-bed lathe for long shafts) calculate verified cutting cycle times, size hydraulic chuck clamping forces, and quote a complete turnkey package without hidden tooling revisions.
Summary
- · Provide both 2D PDF drawings (for tolerances and surface finish) and 3D STEP files (for collision and toolpath simulation).
- · Specify raw material condition and hardness so engineers can match spindle torque and turret station rigidity.
- · State annual batch volumes to determine whether manual loading, bar feeders, or gantry automation delivers the best ROI.
1. Why Incomplete RFQs Delay Machine Tool Procurement
When sourcing industrial CNC machinery, requesting a generic price list without application context often leads to mismatched equipment. A machine quoted without reviewing part geometry may lack sufficient spindle torque at low RPM, adequate through-spindle bar capacity, or high-pressure coolant needed to break stringy alloy chips.
By sharing seven fundamental engineering inputs upfront, your team enables our application engineers to deliver a complete, guaranteed proposal, including machine configuration, cycle-time estimation, and clamping concept, within 24 hours.
All technical drawings and STEP files submitted to Taikan Machine are processed strictly for internal cycle-time and fixture engineering and can be covered by a mutual Non-Disclosure Agreement prior to transmission.
2. The 7 Core Parameters Required for Turnkey Sizing
Before submitting your Request for Quotation (RFQ), consolidate the following part and production metrics:
| Parameter | Required Details | Engineering Impact on Machine Selection |
|---|---|---|
| 1. Part Geometry | 2D PDF with GD&T + 3D STEP file | Determines X/Z or X/Y/Z travel, swing diameter, and tool interference clearance |
| 2. Material & Hardness | Alloy grade, heat treatment state (e.g., 42CrMo4, 45 HRC) | Dictates spindle torque curve, guideway type (roller vs box), and insert grade |
| 3. Blank Condition | Saw-cut bar, cold forging, sand casting, or pre-machined | Determines hydraulic chuck jaw geometry, clamping pressure, and roughing depth |
| 4. Critical Tolerances | IT grade, concentricity, and surface finish (Ra µm) | Defines thermal compensation needs, spindle bearing class, and probing options |
| 5. Target Output | Monthly/annual volume, shift schedule, target cycle time | Balances single-spindle vs multi-machine cell and bar feeder automation ROI |
| 6. Workholding Preference | 3-jaw chuck, collet nose, custom fixture, or tailstock | Sizes hydraulic cylinder bore, drawtube diameter, and programmable tailstock thrust |
| 7. Factory Utilities | 3-phase voltage/frequency, shop air pressure, floor space | Ensures transformer matching, chip conveyor exit direction, and footprint fit |
3. Matching Part Families to the Right Machine Platform
Once our engineering team reviews your checklist, we map each part family to the most cost-effective machine architecture in our lineup:
- · Precision Bushings, Fittings & Flanges (< Ø360 mm): Matched to the TCK50 or TCK52 slant-bed CNC lathe with 45° roller ways and rapid 12-station hydraulic turret.
- · Heavy Gears & Large Bearing Rings (up to Ø420 mm): Matched to the TCK56 heavy-duty slant-bed lathe with a 10-inch hydraulic chuck and 15 kW high-torque spindle.
- · Long Shafts, Rollers & Cylinders (750–3000 mm): Matched to the CK6140, CK6150, or CK6160 flat-bed CNC lathe with box guideways and steady rest support.
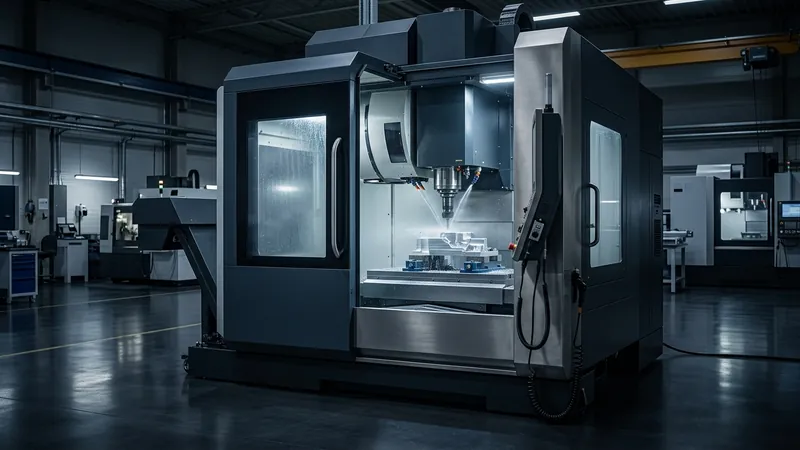
- · Prismatic Housings, Manifolds & Mold Plates: Matched to the VMC650, VMC850, or VMC855 vertical machining center with 24-tool arm ATC and rigid tapping.