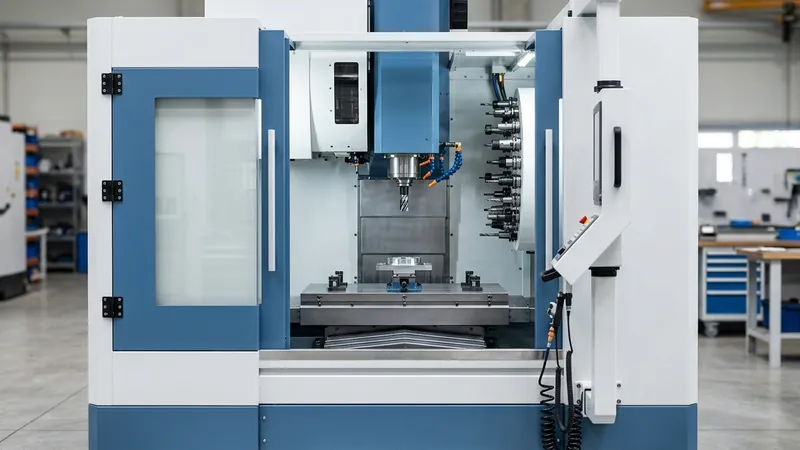
Although the model numbers VMC850 and VMC855 appear to differ by only 50 mm of Y-axis travel (850 × 500 × 550 mm vs. 850 × 550 × 550 mm), the Taikan VMC855 is a fundamentally heavier structural platform built for mold bases and hard alloy roughing. While the standard VMC850 (5,600 kg net weight) uses 35/35/45 mm roller linear guideways, Ø32/40 mm ballscrews, and an 11/15 kW BT40 spindle optimized for rapid contract machining and aluminum/steel production, the VMC855 upgrades the frame to 6,500 kg (+900 kg of Fine-Grain HT300 cast iron), equips 45/45/45 mm heavy roller guideways and Ø40 mm C3 ballscrews on all three axes, expands table load capacity from 600 kg to 800 kg, and fits a Ø150 mm BBT40 dual-contact spindle rated at 15/18.5 kW (118 Nm torque) with ±0.003 mm positioning accuracy.
Summary
- · The VMC855 is not merely a stretched VMC850, it adds 900 kg of cast-iron column and saddle mass and upgrades X and Y axes from 35 mm to 45 mm roller linear guideways (+42% dynamic load rating).
- · Select the VMC850 for high-mix contract machining, automotive aluminum die-castings, hydraulic manifolds, and 4th-axis rotary production where 36 m/min agility and lower capital cost maximize ROI.
- · Select the VMC855 for P20/H13 injection and die-casting molds, forging dies, and heavy interrupted face milling requiring a Ø150 mm BBT40 dual-contact 15/18.5 kW spindle.
1. Why 50 mm of Extra Y-Axis Throat Requires a 900 kg Heavier Column
In a C-frame vertical machining center, extending the Y-axis travel from 500 mm to 550 mm increases the spindle overhang distance from the front face of the column. Without a structural redesign, a longer throat would amplify bending moments during Z-axis plunging and heavy face milling.
To eliminate overhang deflection, the Taikan VMC855 widens the A-frame column base, deepens the saddle casting, and increases total machine mass from 5,600 kg (VMC850) to 6,500 kg. Furthermore, all three axes (X, Y, and Z) are equipped with 45 mm roller linear guideways and Ø40 mm C3 pretensioned ballscrews.
Standard BT40 toolholders contact only the 7:24 spindle taper, leaving a 2–3 mm gap at the flange face. The VMC855 uses BBT40 dual-contact tooling that seats simultaneously against the taper and the Ø150 mm spindle nose face, increasing radial tool stiffness by 30%.
2. Side-by-Side Technical Comparison: VMC650 vs. VMC850 vs. VMC855
Review the exact engineering specifications across our three vertical machining center platforms:
| Specification | VMC650 (Compact High-Speed) | VMC850 (Flagship Production) | VMC855 (Heavy Mold & Die) |
|---|---|---|---|
| X / Y / Z Travel | 650 × 400 × 500 mm | 850 × 500 × 550 mm | 850 × 550 × 550 mm |
| Table Size & Max Load | 800 × 400 mm (400 kg) | 1000 × 500 mm (600 kg) | 1000 × 550 mm (800 kg) |
| Spindle Taper & Speed | BT40 · 12,000 rpm Direct | BT40 · 10,000 rpm (12k Opt.) | BBT40 Ø150 mm · 10,000 rpm |
| Spindle Motor Power | 7.5 / 11 kW | 11 / 15 kW | 15 / 18.5 kW (118 Nm) |
| Roller Guideways (X/Y/Z) | 35 / 35 / 35 mm | 35 / 35 / 45 mm | 45 / 45 / 45 mm |
| Positioning / Repeatability | ±0.003 / ±0.002 mm | ±0.004 / ±0.002 mm | ±0.003 / ±0.0015 mm |
| Machine Net Weight | 4,200 kg | 5,600 kg | 6,500 kg |
3. Application Decision Framework: Which VMC Should You Quote?
If 70%+ of your spindle hours involve aluminum alloys (6061, 7075, A380 die-castings), mild carbon steels, stainless steel plates, or 4th-axis fixture work under 600 kg, the VMC850 delivers identical rapid traverse speeds (36/36/32 m/min) and 1.8-second ATC tool changes at an ~11% lower machine investment.
If your shop machines pre-hardened P20/718 mold bases, H13 hot-work die blocks, or uses Ø63–Ø80 mm indexable face mills at deep axial engagement, the VMC855 pays back its price differential within 4 to 6 months through 25% faster roughing metal removal rates (MRR) and 30% longer carbide insert life.